

MEMS metal components are the precision hardware around a finished die: lead frames, lids, hermetic-seal parts, carriers, test sockets, and assembly tooling. They require tight geometry, clean edges, controlled material condition, and reliable registration through packaging and test.
This guide focuses on those metal packaging components and production tools. It does not cover wafer fabrication, MEMS foundry work, or silicon-die processing; it explains the mechanical hardware that protects, connects, handles, and tests the device after the die exists.
MEMS Process Boundaries: Die Fabrication vs. Metal Hardware
It helps to separate MEMS manufacturing into the steps that build the die and the steps that package, test, and handle it. The two need entirely different supply chains, and confusing them wastes time on both sides.
Silicon Die Fabrication: Outside This Guide
The front end creates the moving silicon structure on a wafer. As a Carnegie Mellon overview describes, the common techniques are bulk micromachining, wafer-to-wafer bonding, surface micromachining, and high-aspect-ratio micromachining. None of this is metalwork; it is cleanroom semiconductor processing, and it sits outside a laser-microfab shop's scope.
Metal Packaging, Assembly, and Test Hardware
Once the die exists, it has to be protected, connected, handled, and tested. This back-end stage is full of precision metal parts and tooling — packages, interconnects, carriers, sockets, and fixtures. It is also where much of a device's cost and many of its reliability problems live.
Where Precision Laser Micromachining Fits
Precision laser micromachining supports the metal hardware around the die: package and interconnect components, handling carriers, test sockets, and assembly fixtures. The work begins after the silicon device process and focuses on fit, edge condition, heat control, material compatibility, and measurement evidence.
Tooling and fixturing for MEMS assembly and test
Before the metal that ships inside a device, there is the metal that builds it: the tooling. Production tooling rarely gets discussed, yet it sets throughput and yield on an assembly line.
Handling and transport carriers
Die and packaged parts move through assembly in metal carriers and trays that locate each part precisely. Loose fit causes misplacement and damage, while tight, repeatable pockets protect yield. These carriers are thin metal parts with many identical features held to a common datum.
A carrier also has to survive repeated automated loading without wear that shifts those features. That favours a stable alloy and a clean, accurate cut over a low-cost approximation.
Test sockets and probe-card hardware
Electrical test needs metal hardware that contacts each device in the same place every time. Precision sockets and probe-card components position contacts to tight tolerance across a full array. Worn or misaligned test hardware shows up directly as false failures and lost yield.
Because test touches every unit, this hardware runs at the full throughput of a MEMS manufacturing line, so its accuracy compounds across the entire production volume. A small registration error there becomes thousands of mis-tested parts.
Assembly jigs and process fixtures
Bonding, sealing, and inspection steps each need a jig that holds the part flat and located. A custom fixture turns a manual step into a repeatable one. Because every device geometry differs, these jigs are non-standard metal parts made to order.
A well-made jig also de-skills a delicate step, letting an operator place and hold a part the same way every cycle. That repeatability is often what stabilises early yield.
Metal package and interconnect components
The parts that ship inside the finished device are the second metal category. We cover the device-side components in depth in our guide to metal components for MEMS sensors, so this section stays brief.
Lead frames at production volume
A lead frame carries connections from the die outward and supports the package through assembly. At volume, the priorities are burr-free edges, flatness, and consistent feature-to-feature registration. Small defects multiply across thousands of parts.
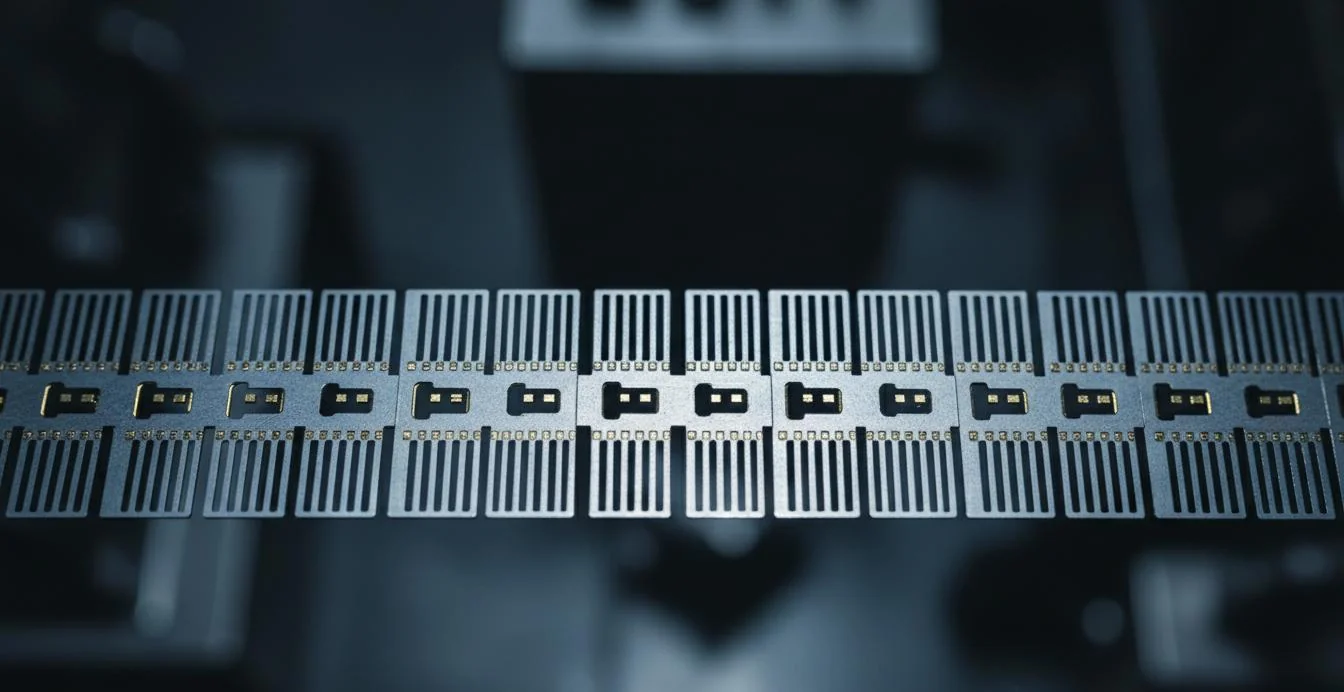
At MEMS manufacturing volumes, the cost of a defect is the cost of every downstream step already spent on that part. Edge and flatness control on a lead frame therefore pays back well beyond its unit price.
Lids, caps, and shields
Many MEMS devices sit in a sealed cavity closed by a metal lid or cap, sometimes inside an electromagnetic shield. These are thin, formed or cut metal parts whose fit decides the seal. Edge quality and dimensional consistency carry straight into reliability.
A lid that warps or sits proud also disturbs the parts stacked above it, so flatness is checked alongside the outline.
Hermetic and CTE-matched parts
Hermetic packages join metal to glass or ceramic, so the metal's coefficient of thermal expansion (CTE) must match across the joint. A NASA packaging review notes that metal packages reach a hermetic glass-to-metal seal by glass firing, and Fraunhofer IZM's hermetic-packaging work relies on precisely formed metal bond frames. The alloys for this — Kovar and Invar — are machinable to the tolerances below.
Why Laser Micromachining Suits MEMS Metal Components

Laser micromachining removes metal with a focused beam, with no die or mask. For these parts and tooling, that brings three concrete advantages and one trade-off.
No tooling, prototype to production
Because there is no mould, a part moves from CAD to finished metal directly, and the first piece and the hundredth cost about the same. MEMS programs iterate hardware between builds, and a drawing change then costs no tooling time. The same process carries a part from prototype into low- and mid-volume production.
Across a MEMS manufacturing program, that flexibility compounds, since each design spin avoids both a tooling charge and a tooling lead time. The metalwork then rarely sits on the critical path during a ramp.
Feature sizes below etching and stamping floors
Laser cutting reaches features that mechanical and wet processes cannot. Stamping is generally limited to holes near 1.0 mm and CNC punching to about 0.5 mm, while chemical etching needs a minimum hole near 1.5 times the material thickness. Laser micromachining produces holes far smaller than the sheet thickness, down to a 0.02 mm minimum.
Heat-affected zone and burr control
A laser is a thermal process, so it leaves a heat-affected zone, or HAZ — a narrow band near the cut where the metal's structure has changed. On parts that sit beside a fragile die, this must be controlled, and the HAZ here is held within 0.05 to 0.2 mm. Edges are produced burr-free, since a loose burr near a die is a defect.
Tolerances for Automated MEMS Assembly Hardware
MEMS assembly is automated, and automation is unforgiving of variation. A part that fits a person's hand may still jam a feeder, so the numbers matter more than they look.
Registration and fit for automated handling
Pick-and-place and automated feeders rely on each part presenting features in the same place. Feature-to-feature registration across a part is held by CCD vision positioning at ±0.005 mm. Consistent registration is what keeps an automated line from stalling.
Achievable tolerances and feature sizes
Machining accuracy runs from ±0.005 mm to ±0.02 mm, with a minimum hole diameter of 0.02 mm, minimum line width of 0.015 mm, and kerf — the width of the cut — down to 0.01 mm. Those figures define which geometries are feasible before a design is committed. The tighter end of the range sits near the capability limit and warrants a first-article check.
These figures also bound what is realistic to request, since a tolerance tighter than the process holds adds cost without improving the part. Specifying to the capability keeps cost and quality aligned.
Edge quality and contamination control
Surface roughness runs Ra 0.8 to 3.2 µm depending on material and thickness, and edges are burr-free. On a production line, a single particle or burr near a cavity or bond pad can scrap a device. Deburring and full surface-quality inspection address this.
Cleanliness expectations also rise with the assembly environment, so parts bound for a controlled area may need handling and packaging beyond a standard cut. Confirm those requirements at the quoting stage.
Materials for MEMS Metal Components
Material choice for MEMS hardware is driven by sealing, thermal behaviour, and electrical function. The relevant alloys are all in the machinable set, so the choice is an engineering decision.
Hermetic and low-expansion alloys
Kovar (4J29) and Invar (4J36 and 4J42) are controlled-expansion alloys used where metal meets glass or ceramic in a hermetic package. Matching expansion across the joint keeps the seal intact through thermal cycling. Both machine cleanly at the tolerances above.
Stainless and copper
Stainless steels — 304, 316, and 430 — cover structural, corrosion-resistant, and magnetic functions, with 316 the medical and corrosion grade. Copper and copper alloys serve where electrical or thermal conductivity is needed. Copper's high conductivity calls for controlled thermal diffusion during cutting.
Refractory metals
For high-temperature parts and certain test hardware, refractory metals such as molybdenum and tungsten thin sheets are machinable. They hold up where stainless would not. Material selection should be confirmed against the specific seal, temperature, and electrical requirement.
Because these metals are harder to cut cleanly, a sample run confirms edge quality and dimensional control on the specific grade before a production commitment.
How to Specify MEMS Metal Parts and Tooling
A clear request turns a concept into a correct first article and a predictable ramp. A few specifics make the first article and production ramp more predictable.
Separate the die-side parts from the tooling
Separate items that ship inside the device from production tooling, since the two carry different tolerance and finish priorities. A lead frame has different critical features than a handling carrier. Grouping them correctly avoids over-specifying tooling and under-specifying product.
Give datums, critical dimensions, and material
Provide a drawing with a clear datum, mark the critical dimensions, and name the alloy and sheet thickness. Thickness sets the achievable hole size and influences the heat-affected zone, so it is not a detail. If a hermetic seal or a magnetic function is in scope, say so, because it narrows the material.
Plan for prototype-to-production and traceability
State the expected volumes and whether lot traceability is required, so the right inspection and documentation are set from the first sample. For automated assembly, call out the features that must register for feeders and pick-and-place. Ask for a first article on any part with a critical fit.
Quality and Reliability Risks in MEMS Metal Hardware
The metal parts in MEMS manufacturing fail in ways that trace straight back to how they were cut and finished. Knowing the failure modes is what separates a part that merely fits from one that holds up across a production run.
Particles and burrs near the die
A loose particle or a stray burr from a poorly cut part can land on a die or a bond pad and scrap the device. The risk is highest for parts that sit inside the cavity or contact the die during assembly. Burr-free edges and post-cut inspection are not cosmetic here, because they protect yield directly.
Seal and seam integrity
Hermetic devices depend on an unbroken seal, and the metal seal parts have to fit without a gap. A dimensional error on a lid or seal ring leaves a leak path that a humidity or fine-leak test will later catch. Holding the fit tolerance on these parts is what keeps the seal sound through thermal cycling.
Tooling wear and placement drift
Production tooling degrades, and a worn carrier or socket slowly shifts where parts land. That drift appears as rising misplacement or false test failures over a run, often without an obvious cause. A stable alloy, a clean cut, and periodic re-inspection of tooling keep placement repeatable.
Frequently asked questions
Not the wafer fabrication — the silicon die is built in a semiconductor cleanroom by lithography, deposition, and etching. a precision metalwork provider handles the metal side: package and interconnect components such as lead frames and lids, hermetic-seal parts, and the production tooling — carriers, test sockets, assembly jigs — that moves and tests the device. In short, the metal hardware around the die, not the die itself.
Machining accuracy of ±0.005 mm to ±0.02 mm covers most package and tooling parts, with CCD vision positioning at ±0.005 mm. For automated assembly, feature-to-feature registration across the part matters as much as any single dimension, because feeders and pick-and-place rely on consistent placement. Validate the tightest dimensions on a first article, since they sit near the capability limit.
Kovar (4J29) and Invar are controlled-expansion alloys for hermetic glass-to-metal seals. Stainless steels (304, 316, 430) cover structural, corrosion, and magnetic needs, while copper and copper alloys handle conductive parts. Refractory metals such as molybdenum and tungsten suit high-temperature hardware. The right choice depends on the seal, temperature, and electrical requirement.
For small features, laser usually wins. Chemical etching needs a minimum hole near 1.5 times the material thickness, so on thin foil it cannot reach the smallest openings, and it adds wet chemistry to the flow. Laser micromachining produces holes far smaller than the sheet thickness with better dimensional consistency and no mould. Etching can still suit very large open-area patterns.
Yes. With no tooling, prototypes and low-volume runs are economical, and a simple prototype can arrive in as little as three hours. The same process scales into mid-volume production, under ISO 9001 with full-lot traceability. That lets one controlled process route carry a part from the first sample through a production release.
Conclusion
MEMS manufacturing is two supply chains, not one: the cleanroom that builds the die, and the precision metalwork that packages, connects, tests, and handles it. Laser micromachining belongs firmly in the second — the lead frames, lids, hermetic-seal parts, carriers, sockets, and jigs that a production line runs on, made to micron tolerances without tooling cost at low volume.
The process boundary is deliberate: this guide addresses precision metal parts around the die, not silicon wafer fabrication or MEMS foundry processing. Specify the part function, material, datums, and fit requirements so the correct metal process route can be selected.
For production requirements, see our MEMS laser micromachining services for metal package components, fine features, and feasibility considerations.